Mineral recovery efficiency is one of the more consequential variables in mining economics, and the gap between what a flotation circuit is theoretically capable of recovering and what it actually recovers under real operating conditions is where significant value disappears without ever appearing clearly on any report. Ore grades are declining in many established South African operations, the mineralogy of what is being fed to flotation circuits is becoming progressively more complex, and the water and energy inputs required per tonne of product are increasing as a direct consequence. Flotation solutions in South Africa developed with genuine understanding of the region’s specific ore types, water chemistries, and operational constraints produce recovery improvements that generic reagent and equipment approaches consistently fail to deliver — not because the generic approaches are technically inferior in principle, but because they were not designed around the specific problems they are being asked to solve.
What Recycled Process Water Is Doing to Flotation Performance
The progressive shift towards process water recirculation across South African flotation operations — driven by water scarcity, regulatory requirements, and operational water balance management — has introduced a category of flotation performance variability that many operations have not fully characterised or connected to its source. Recycled process water carries dissolved ions, reagent residuals, and pH variability that were not present in fresh water circuits and that interact with flotation reagents in ways that shift the reagent package’s effective behaviour without the change being visible in the reagent addition rates being reported. Flotation solutions that treat water chemistry as an integrated variable within the flotation system rather than as a separate water treatment problem produce more consistent recovery across varying water quality conditions rather than accepting performance variability as an unavoidable feature of water recirculation.
Cell Hydrodynamics and What They Determine
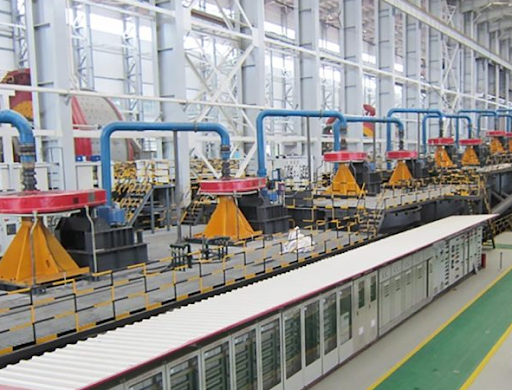
The flotation cell’s geometry, impeller design, and air dispersion system determine the quality of contact between air bubbles and mineral particles that is the fundamental mechanism of the process, and equipment selection decisions made without specific consideration of a particular ore’s liberation characteristics and required bubble size distribution consistently result in circuits that are mechanically functional but hydrodynamically suboptimal. The range of flotation cell designs available to South African operations — from conventional mechanical cells through column flotation to more recently developed designs with enhanced contact mechanisms — suit different applications in ways that general performance claims do not capture, and the selection process benefits substantially from direct experience with similar ores in similar operational contexts rather than from equipment specifications that were developed for different applications.
Circuit Configuration and Feed Variability
Operating mines generate continuous variability in feed grade and mineralogy as the ore body is developed across different areas, depths, and geological domains, and the circuit configuration determines how effectively the flotation plant handles this variability rather than simply performing well under the steady-state conditions that testwork programmes tend to favour. The arrangement of rougher, cleaner, and scavenger stages; the intermediate product recycling strategy; and the points at which concentrate and tailings streams are taken all affect how robustly the circuit maintains recovery when feed conditions shift from the design basis. Flotation solutions in South Africa that include circuit audit and optimisation alongside reagent and equipment supply give operations systematic analysis of where configuration is limiting recovery, often identifying opportunities for improved performance through routing changes rather than additional capital expenditure on cell capacity.
Process Control and the Variability It Manages
The gap between a flotation circuit’s potential performance and its actual continuous performance is substantially determined by the quality of the process control that keeps the circuit operating near its optimum point as feed, reagent supply, and water chemistry shift across shifts and across the operating day. Manual control of large flotation circuits — operators managing froth appearance, pulp levels, air rates, and reagent additions across many cells simultaneously — produces results that are adequate on average and highly variable around that average, and the troughs of that variability represent genuine recovery losses that rarely get attributed to process control rather than to feed variability or reagent performance. Real-time instrumentation that provides direct measurement of froth characteristics, air dispersion quality, and reagent effectiveness creates the feedback that moves control from reactive adjustment toward something that actually maintains performance.
Technical Support and Why Proximity Matters
Technical support for flotation operations delivers substantially different value depending on how specifically it engages with the conditions of the actual operation and how quickly it can respond when something is not performing as expected. The solution that addresses a recovery problem in a Bushveld platinum circuit has no guaranteed relevance to a similar-appearing problem in a Witwatersrand gold operation, and technical support that understands these differences from direct experience with similar South African operations in comparable contexts is consistently more useful than remote support applying a generic diagnostic framework to a situation it is encountering at a distance. On-site testwork capability, rapid reagent trial capacity, and the ability to monitor and interpret circuit response to changes in real time rather than across the turnaround time of international logistics produce operational outcomes that remote technical support cannot match.
Conclusion
Flotation solutions in South Africa that engage genuinely with the ore-specific, water-specific, and operationally-specific challenges of individual mining operations produce recovery improvements that generic approaches consistently leave unrealised. The combination of application-specific reagent chemistry, appropriate equipment selection, circuit configuration analysis, and local technical capability that understands the specific conditions of South African mining creates a foundation for sustained performance improvement that becomes more valuable as ore grades continue to present increasing challenges to flotation circuit performance.